Applications · Electrical Enclosure · Steel Sheet
The installation decides the sheet.
An enclosure is specified by where it stands and what it has to keep out, not by the box it becomes. The exposure decides the coating, the fold and cut-out pattern decides how the sheet has to behave at the brake and the punch, and the earthing and glanding details decide which edges must stay clean and continuous. Pick the sheet before those three are settled and you are buying material against a drawing that does not exist yet. This page starts from the enclosure's build intent and works back to the sheet the order has to name.
Send the enclosure’s exposure, how the case is formed, and where the finish comes from. Pricing is on request — no rate is published before the coating route is named.
A protection class belongs to the assembled enclosure. The sheet supplies the substrate it is built from — and the shape it holds.
Exposure
What the coating is chosen against
Fabrication
Folds, cut-outs and welded joints
The finished assembly
Where the protection class, the bonding and the testing actually live.
What The Enclosure Requires
Four things about the enclosure that decide the sheet
An enclosure drawing shows a box. The values that actually choose the sheet sit beside it — in where the box stands, how it is folded and opened, what it has to keep out, and how it connects into the installation.
Where the enclosure stands
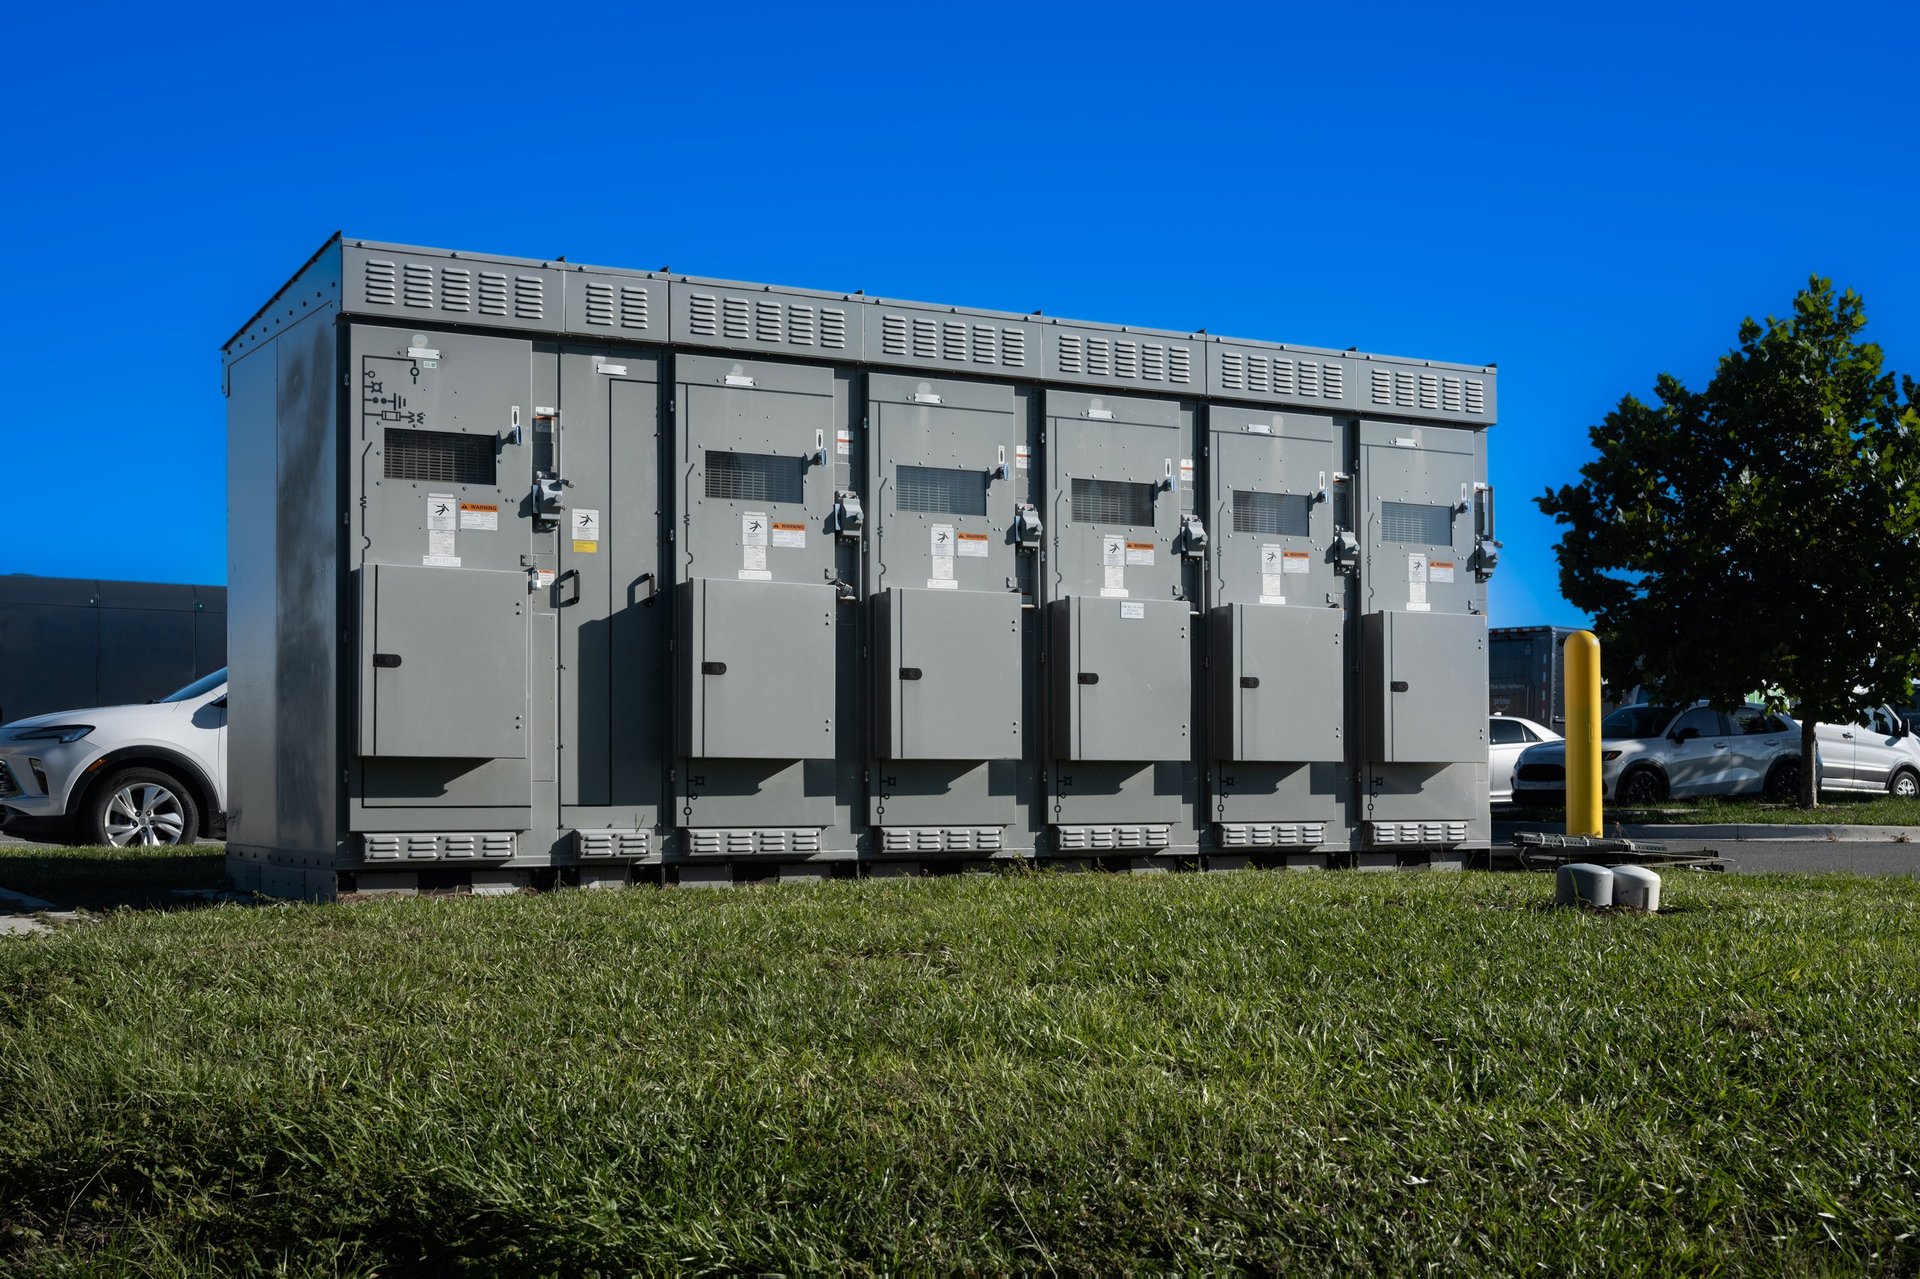
An indoor cabinet on a plant floor, a rooftop unit, a roadside kiosk and a coastal installation are four different corrosion duties on the same box. The exposure is decided by the site and the client's specification long before the sheet is chosen, and it is what a coating is actually selected against.
Exposure is the first question because it drives the coating, and the coating drives which substrate is worth buying. An indoor and an outdoor enclosure of identical size are frequently two different sheet specifications.
How the case is folded and cut
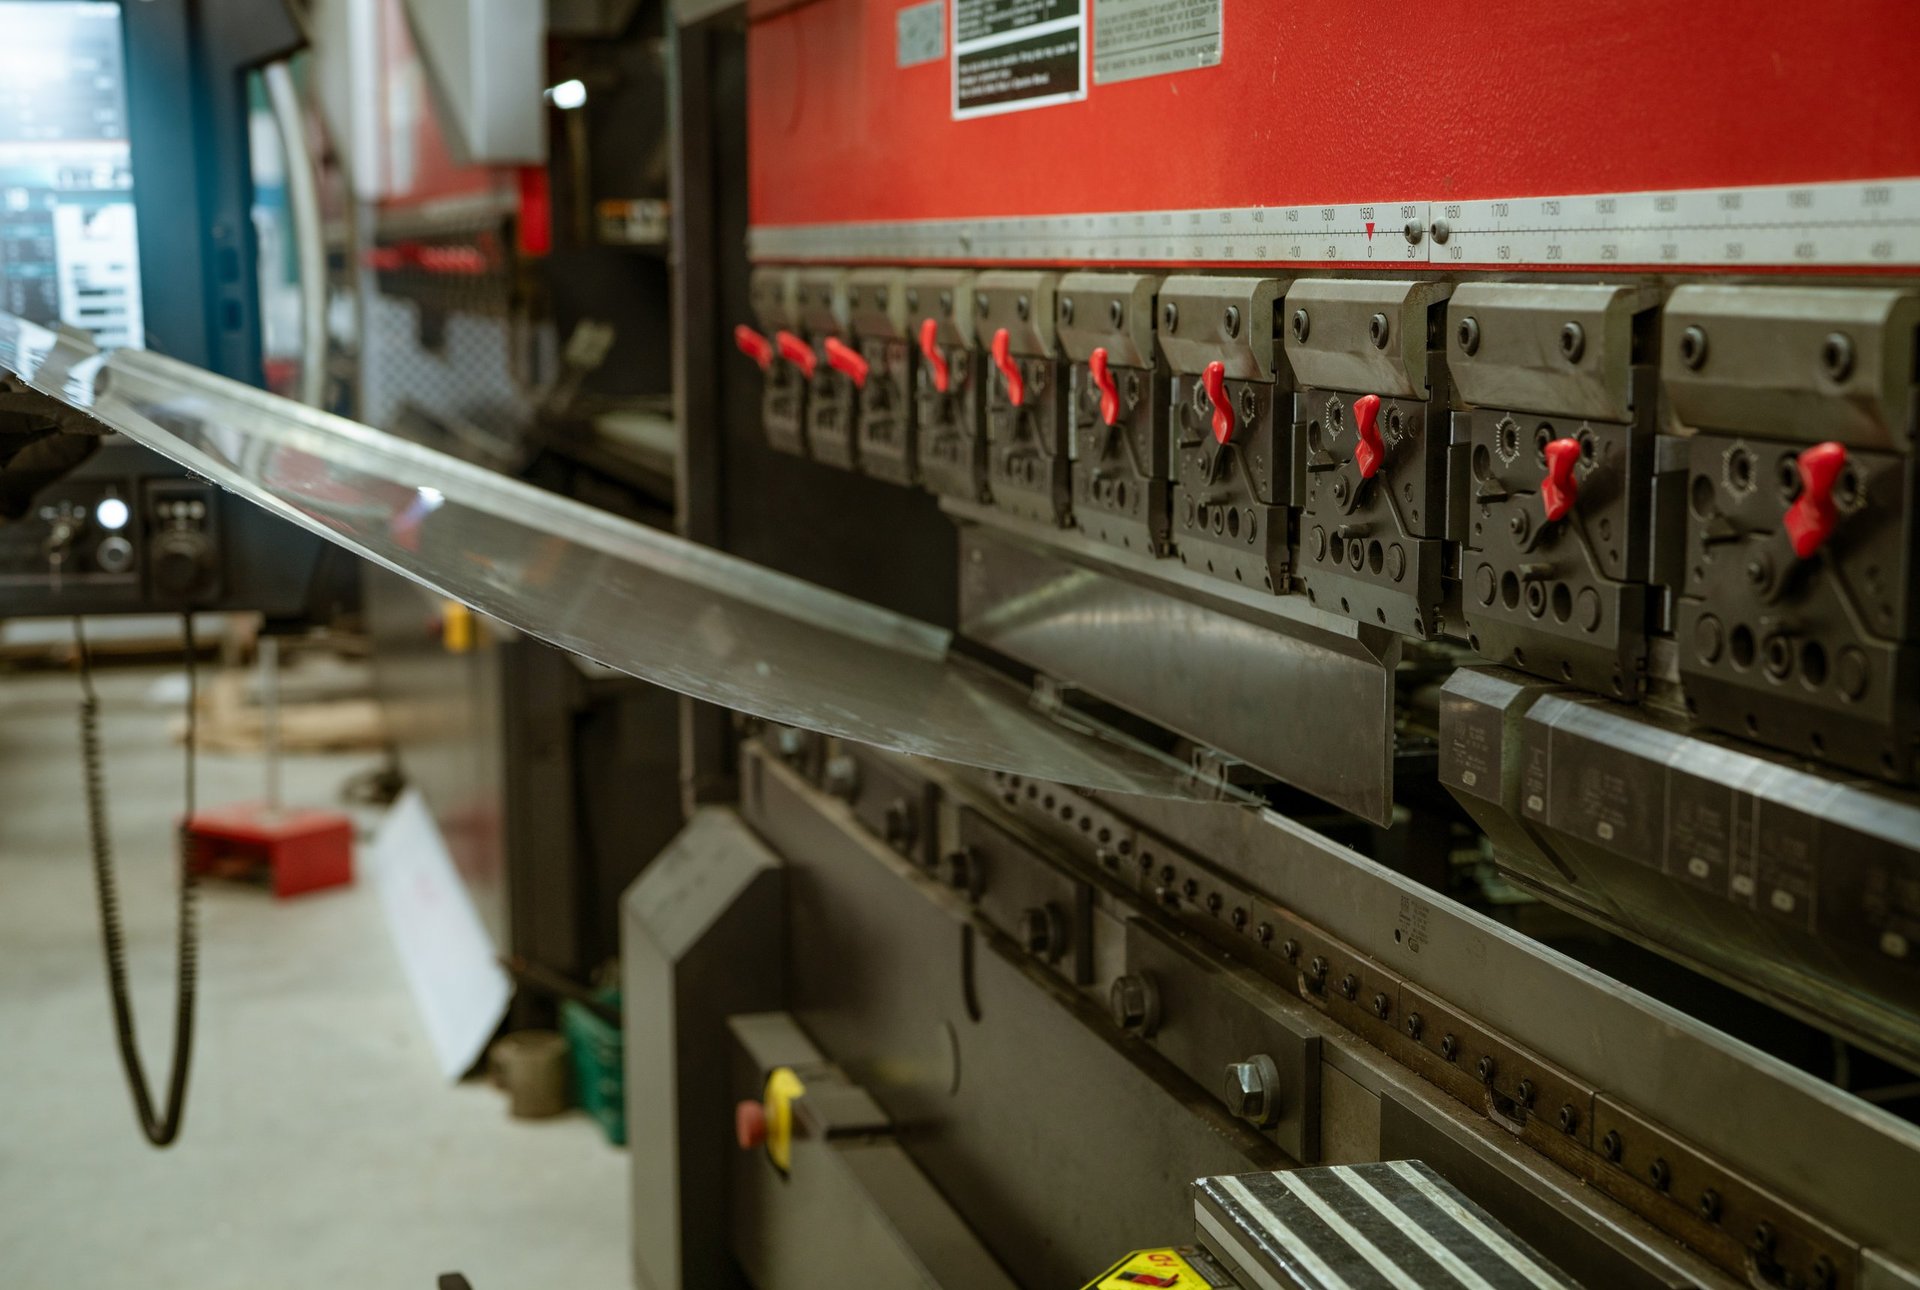
Enclosure bodies are press-braked from flat blanks into a box with returns, stiffening flanges and often a turned lip on the door. Door cut-outs, gland plates, mounting holes and ventilation apertures are punched or laser-cut. Each of those operations puts its own demand on the sheet.
The bend pattern and the cut-out layout come from your own tooling and drawings. They set the ductility the sheet needs at the fold line and the edge condition the assembly needs at every opening — neither of which is implied by the sheet's name.
What the finished assembly must keep out
Enclosure protection is expressed as a class or rating the assembled cabinet must achieve — dust, water, impact, and where relevant the requirements of the electrical installation standard the project applies. That rating belongs to the finished fabrication: the gasket, the door geometry, the seal, the hardware and the workmanship together.
A sheet of steel does not carry a protection class, and no sheet supplier can confer one. What the sheet can do is give the fabricator a flat, consistent, formable substrate so the sealing geometry in the design behaves as drawn.
Earthing, bonding and glanding details
An enclosure is part of an electrical installation, and its metalwork is used for bonding and for the mounting of glands, earth studs and conductive fixings. Those details are settled by the electrical design, not by the sheet order.
Bonding continuity is an assembly property, established by the finished enclosure and its installation. The sheet's contribution is that the surfaces where bonds and glands land are sound, clean and predictable.
Why a protection class cannot be bought with the steel
A class or rating describes what an assembled enclosure keeps out — dust, water, impact — and it is demonstrated on the finished product, by test, under the standard the project applies. Every element that earns it belongs to the fabrication: the door geometry, the gasket and its compression, the seal around cable entries, the hardware, and the consistency of the work that assembles them. A sheet of steel has no class to give, and no distributor can confer one.
What the sheet has to do is support that design rather than fight it. A flat, consistent, formable substrate holds the fold and the closure geometry the drawing specifies, and it lets the gasket land on the surface it was dimensioned for. That is the honest contribution of the material to an enclosure rating — real, worth specifying, and not the same thing as the rating itself.
Enclosure Build Intent
Describe the build, and watch the sheet dependencies fall out
Five questions about the enclosure you are building. Each answer sets a field on the enquiry and raises the combinations that cannot be left open. Nothing is calculated and no rating is produced — the selector collects what the sheet order has to carry.
Where will the enclosure be installed?
Three coating routes, and what each one is chosen against
Metallic-coated sheet (galvanized)
Protection that comes from a metallic coating on the steel, chosen where the enclosure will meet moisture or a mildly aggressive atmosphere. The coating protects sacrificially, which is why it keeps working at the cut edges, punched openings and fold lines that every enclosure is full of.
Judged on: Whether the substrate behind the coating is protected at the edges and openings the fabrication creates, not only on the flat.
Prepainted sheet (PPGI)
A coated sheet carrying a paint system on top of the metallic coating, adding colour and an appearance requirement. It suits enclosures that will be seen, or that take on a client's colour standard.
Judged on: The finished appearance on the flats, balanced against the reality that the paint reaches only the surfaces it was applied to.
Uncoated sheet, finished after fabrication
A substrate bought for forming and finish adhesion, with the surface treatment applied at your own plant after folding, welding and cutting are done. The protection follows the fabrication rather than arriving with the material.
Judged on: Whether the pre-treatment and the coating reach into the folds, seams and openings — the places a post-fabrication finish can miss.
This enclosure’s build intent
- Location
- Fabrication
- Coating route
- Edges
- Assembly
Still to answer: Location, Fabrication, Coating route, Edges, Assembly.
No grade, thickness or coating is recommended here, and no protection class is attributed to the material. Forming behaviour is established at your brake; the class belongs to the finished assembly.
Choosing The Sheet
Match the sheet to the enclosure, not to the name of the metal
Enclosure fabricators work from a small number of material routes, and the split is driven by exposure and by where the finish is applied. Each route below is a starting point — the grade, the thickness, the flatness and the edge condition are the fields the order actually carries.
Indoor enclosures
The corrosion duty is light, so the binding requirements are fabrication and finish. The sheet is chosen for how it folds, how it takes a cut-out, and how it holds the closure geometry — with a finish that suits the plant it sits in.
Outdoor and coastal enclosures
Exposure takes over the specification. The material route has to protect the places an enclosure is made of — edges, openings and fold lines — and the treatment of those edges becomes a build decision rather than a detail.
Where the finish is applied changes which substrate is worth buying
If the finish is applied at your plant after fabrication, the sheet is bought for forming and for how well it takes that finish — including inside the folds and seams your pre-treatment has to reach. If protection arrives with the material, the sheet is bought for the coating it carries and for how that coating behaves where the fabrication interrupts it. Those are two different purchases, and the drawing rarely says which one it is.
Most outdoor enclosures are built from the metallic-coated route, where the coating keeps protecting the steel at the edges the fabrication exposes — the galvanized steel sheet range sets out what that coating does and where it stops.
Where the enclosure is on show and takes a client colour standard, the prepainted PPGI sheet route covers the coated-and-painted product and its cut-edge behaviour.
Kiosks, canopy elements and weather-shielding on outdoor enclosures often use a profiled form rather than a flat one — the corrugated steel sheet range covers that.
Where enclosure bodies are blanked from coiled stock rather than bought as cut sheets, the upstream form and its handling conditions are in the steel coil range.
A material route is a starting point, not a specification. The grade, the thickness with its tolerance, the flatness and the edge condition are what the enclosure order carries — and none of them is implied by the route’s name.
Writing The Enclosure Scope
The fields an enclosure sheet order carries, and what each one fixes
A sheet order names a product. An enclosure-ready order names the product and the duties the built case puts on it. These are the fields that turn one into the other — and anything absent is decided by whoever quotes the order.
| Order field | What it fixes on the enclosure |
|---|---|
| Installation and exposure | Whether the enclosure is indoor, outdoor or coastal, which is what the coating and the edge treatment are chosen against. |
| Forming and cut-out pattern | How the case is folded and opened up — the brake work, the door cut-outs, the gland plates and the vents. |
| Coating route | Whether protection arrives with the material or is applied by you after fabrication. It decides which substrate is worth buying. |
| Material family and grade | The grade your folding and welding experience requires, confirmed against the standard the drawing cites. This page supplies no grade. |
| Thickness with its tolerance | The band the brake accepts and goods-in verifies. It has to suit the bend radius and the stiffness the door needs. |
| Blank and cut sizes | Whether the order is supplied as flat blanks sized for the brake, as standard sheets to be cut, or to a size your punch accepts. |
| Flatness and edge condition | How the door and the closure surfaces behave, and whether burrs or a rolled edge matter on the exposed openings. |
| Surface condition and treatment | What the surface has to be for finish adhesion and for the bonded and glanded areas of the assembly. |
| Protection through plant and store | How the coated surface is protected between goods-in and fabrication, where handling marks on a visible panel are created. |
| Documents, standard and destination | What is evidenced at dispatch and against which basis, the standard the finished enclosure is built to, and the receiving end. |
No grade, thickness table or coating figure is published here, and no protection class is attributed to the material. Each field is read from the drawing and the standard the project cites.
Releasing enclosure sheet at goods-in
- Confirm the certificate cites the specification with the same edition your order invoked, not the designation alone.
- Check the coating basis recorded against the exposure your order stated — and if no coating requirement was written, that is the gap to close before the sheet is released.
- Compare thickness and flatness against the ordered band, because a blank that will not fold and close consistently will not assemble into a sealing enclosure.
- Inspect the cut edges and any coating damage on arrival, since those are the places corrosion begins and the places your edge treatment has to reach.
Where the enclosure’s own documents sit
The sheet’s record answers one question — what the material is. The enclosure’s protection class, its test evidence and its conformity to the standard the project applies are documents of the finished assembly. They are produced by the enclosure builder and by whoever tests it, and they are not interchangeable with a mill certificate.
What The Record Proves
A material certificate and an enclosure rating are two different claims
An enclosure is accepted by a test on the finished assembly and by the shape of the fabricated case. The material record covers one line of that, and it is worth being precise about which.
What the sheet record establishes
The material the sheet was produced as, its thickness against the standard your order cites, and the coating it carries. Each is a checkable statement about the metal you received.
What it cannot establish
The enclosure’s protection class, its ingress performance or its conformity to an installation standard. Those belong to the assembled and tested product.
Where the enclosure evidence comes from
From the fabricator, the assembly and the test — not from the material supply. A supplier confirms what the sheet is and that it matches the order; whether the enclosure as built keeps out dust and water, and meets the standard the project applies, is a property of the finished cabinet and the process that made it. A distributor cannot confer that, and a mill certificate never claimed to. Keeping the two claims apart is what stops a material record being read as an enclosure rating, which is the misunderstanding most likely to surface late — at commissioning, with the installation already built around the box.
Commercial Basis
What is confirmed against your enquiry, not published in advance
An enclosure order turns on the coating, thickness and blank size together, against the exposure the box will meet. Whether that combination is obtainable is confirmed per enquiry rather than assumed from a product list.
Coating, thickness and blank size together
Whether the combination your enclosure needs is obtainable — the three are checked as one, because the exposure constrains the coating and the brake constrains the rest.
Edge and opening treatment
Whether the cut edges and openings on this build can be left as fabricated, or need a treatment that the order should anticipate.
Reconciliation basis
The figure the order is checked against — by sheet, by blank or by weight — stated so quotations can be compared honestly.
Documents and origin
The dimensional and coating record, and the producing source, stated against the actual enquiry rather than offered as a generic pack.
Pricing is on request. No rate, lead time or stock position is published before the exposure, the coating route and the blank sizes are confirmed.
Related Routes
Where the questions either side of this one are answered
Each of these settles something an enclosure sheet enquiry raises. Open one only when it is the question in front of you.
GCC Supply
Enclosure sheet into the Gulf — quoted against the exposure the box will meet
Enclosure fabrication across this region runs from panel shops building control cabinets through to outdoor and coastal installations where exposure dominates the specification. Each country is planned on its own route, against the requirements the enquiry states.






A country link is a destination-planning page. None of them implies a local office, warehouse or stock position, and none of them changes the requirements on your enclosure order.
Why the protected edge is not the flat surface
An enclosure corrodes at the edge long before the flat face shows anything.
Flat-rolled steel is ordered against product standards that do the same job for every buyer: they define the product, set the ordering conditions, and establish how the material is tested and accepted. Commercial grades are graded at boundaries wide enough to be workable, and a fabricator ordering tonnage normally accepts the product on that basis. What that framework does not do is describe an enclosure, because an enclosure is a fabrication — a box of folds, laps, cut-outs and joints, none of which exist when the sheet is despatched.
That is why the corrosion behaviour of an enclosure has so little to do with the appearance of the flat sheet. Every fold breaks a coating along a line. Every punched hole exposes a cut face. Every lap or welded joint creates a crevice where moisture sits and stays. The protected area of a finished enclosure is the small part of it; the edges, openings and overlaps are what the exposure actually attacks, and they are created by the fabricator rather than supplied by the mill.
The practical consequence is a pair of decisions, and they are worth making together. Where a coating system protects by sacrificing itself at the exposed edge, the sheet tolerates a cut edge and the fabrication can proceed normally. Where protection depends on a barrier film that only exists where it was applied, every cut edge is an untreated route into the steel, and the build has to say how those edges are closed — a touch-up, a sealant, a rolled edge, or a design that keeps them out of the weather. Leaving that question open does not remove it; it moves it to commissioning, when the enclosure is already installed and the correction is at its most expensive.
None of this is a statement about any enclosure’s protection class. A class is earned by the assembled and tested product. What the material contributes is the behaviour at those interrupted places — and that is a property worth specifying deliberately, because it is the one the enclosure will be judged on after a few seasons in service rather than on the day it is delivered.
Why Start From The Installation
What an installation-first sheet order buys the enclosure builder
Fixing the exposure and the edge treatment before the substrate takes a few more lines on the enquiry. These are the honest terms of that exchange.
The coating is chosen against the site
Once the exposure is on the enquiry, the coating is selected for the atmosphere the enclosure will actually sit in — rather than inherited from the last build or decided by whatever the supplier stocks.
Edge treatment becomes a build decision
Deciding how cut edges and openings are treated turns the enclosure's weakest points into a planned step on the build sheet, instead of a discovery at commissioning.
Compliance stays where it belongs
The supplier confirms the material; the fabricator owns the assembled enclosure and its tested class. Separating those two claims stops a mill certificate being read as an enclosure rating.
How The Order Moves
From the enclosure drawing to a fabrication-ready delivery
Each step settles something the next one depends on. The exposure is fixed before the coating is chosen, and the coating before the substrate is ordered.
- 01
Fix the installation and exposure
Establish where the enclosure stands and what atmosphere it meets. It is the value the coating, and therefore the substrate, resolves against.
- 02
Set the coating route
Decide whether protection arrives with the material or is applied at your plant after fabrication, and let the grade and thickness follow from that.
- 03
Plan the edges and openings
Decide how cut edges, punched openings and joints are treated, and check that against the exposure the enclosure will actually meet.
- 04
Confirm blanks and documents
Match the blank and cut sizes to the brake and the punch, and agree which dimensional and coating records the receiving inspection will check.
Coating availability, thickness-and-blank pairing and producing origin are confirmed against the live enquiry — never inferred from a published list.
Request a QuoteCommon Questions
Questions an enclosure sheet enquiry usually raises
Does the sheet we order determine our enclosure's IP rating?
No, and it is worth being firm about this because the misunderstanding is expensive. A protection class is a property of the assembled enclosure — its door geometry, gasket, seal, hardware, cable entries and the workmanship that puts them together. It is demonstrated by the finished product, usually by testing, under the standard the project applies. Steel sheet has no protection class to give. What a consistent, flat, correctly formed substrate does is let the sealing design you drew behave the way you designed it.
Why do enclosures corrode at the cut edges and holes first?
Because those are the places the protective coating is interrupted. Every punch, cut-out and drill exposes steel that carries no coating on the cut face. On a metallic-coated sheet the surrounding coating continues to protect that exposed steel sacrificially, which is the main reason galvanized sheet is the usual choice for outdoor enclosures. On a paint-only system the cut face is simply bare, so it depends on how the fabricator treats those edges afterwards.
Should we fold first and coat afterwards, or buy pre-coated?
It depends on which problem you would rather manage. Folding first and coating afterwards gives the best coverage of the finished shape, including inside the folds, and it puts the surface treatment under your own control — provided your pre-treatment actually reaches the folds and seams. Buying pre-coated removes the painting step from your line and gives you a consistent factory finish, at the cost of cut edges and formed corners where the film was interrupted. Neither is wrong; the exposure and the appearance requirement usually decide it.
Does the enclosure's earthing depend on the sheet we buy?
Bonding continuity is established by the finished assembly and its installation — the earth studs, the bonded removable parts, the glands and the connections between them. That is an electrical design and assembly question, not a material one. What the sheet contributes is that the surfaces where those bonds land are sound, clean and free of anything that would interfere with a reliable connection. Coating on a mating surface is exactly the kind of detail worth deciding early, because it is awkward to correct after the enclosure is built.
What has to be on an enclosure sheet enquiry?
Whether the enclosure is indoor or outdoor and what atmosphere it will sit in, the forming the case requires, the material family and grade your tooling needs, the thickness with its tolerance, the blank or cut sizes the brake and punch accept, the flatness and edge condition, the surface condition, the quantity, the documents required and the destination. Add the standard or specification the finished enclosure is governed by, even though the sheet does not satisfy it on its own — it tells us what the material is being built into.
Request a Quote
Send the exposure, the fabrication and the coating route
An enclosure sheet enquiry needs the installation's duty and the fields the order carries. Name the exposure, the forming and the coating route, and anything left open comes back as a question rather than an assumption.
Where will the enclosure be installed?
How is the case formed and opened up?
Where does the protective finish come from?
This route is handled through the steel sheet desk. Prefer that page’s form? The same team answers at the main steel sheet enquiry desk.
Specify the installation first, then the sheet under it
Send the enclosure’s exposure, how the case is formed and where the finish comes from. The offer comes back as a sheet scope the enclosure can be built from, with the open questions named rather than assumed.
sales@noordeirasteel.ae · +971 56 398 0860 · Business Bay, Dubai