
Steel Coil · Standard EN 10130
EN 10130 Cold Rolled Coil — Uncoated Forming Feed, and Nothing Else
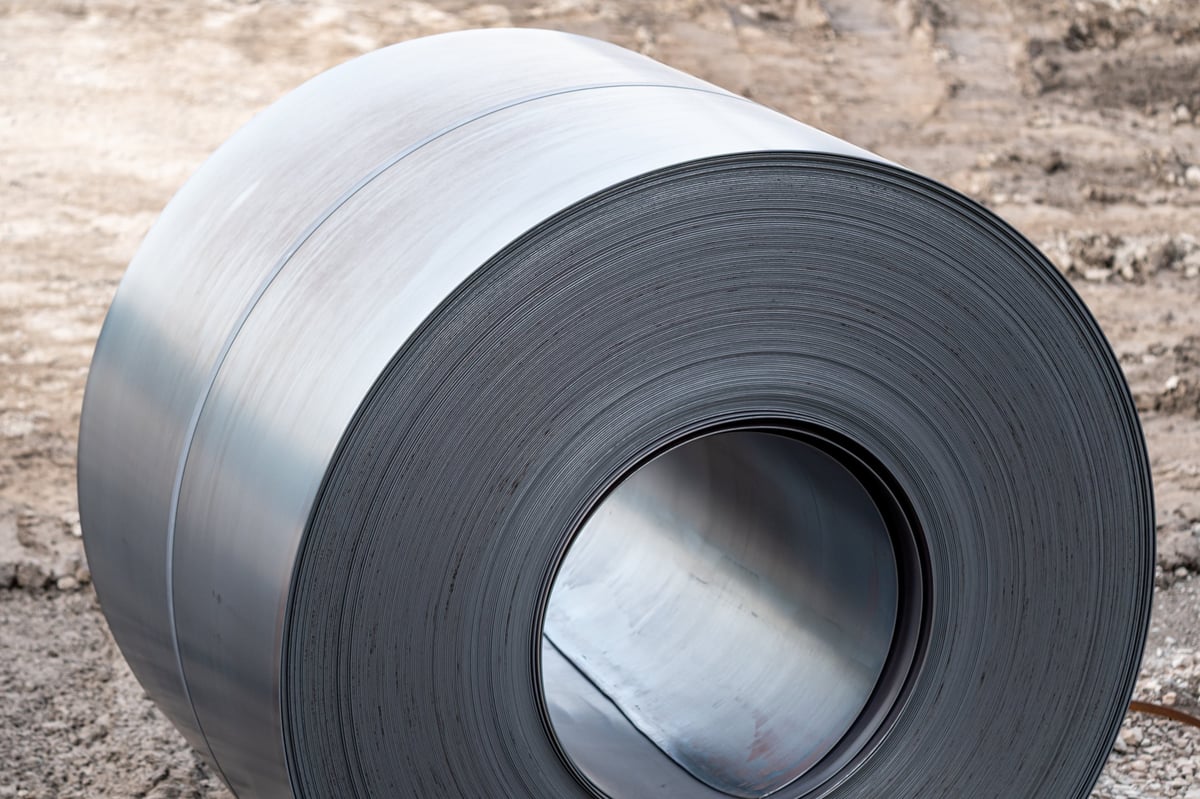
This standard is written for uncoated cold rolled low carbon flat steel intended for cold forming. That single phrase — uncoated, flat, for forming — is the whole qualification. A galvanised or pre-painted coil is not this material, and a cold-rolled strip outside the width the standard addresses is not this material either, however similar it looks on the line.
Price on request · Surface condition and forming grade confirmed before quoting
Uncoated Only
Cold rolled, low carbon, uncoated, and destined for forming
If you are the quality lead releasing cold-rolled feed to a forming line, the standard's applicability check comes before the grade discussion. Four conditions decide whether this is your standard at all.
Cold rolling is a processing route, not a product identity. Two coils can come off the same pickle line and the same mill stand and end up governed by completely different standards, because what decides the applicable document is what happens to the surface afterwards and what the coil is asked to become.
This standard addresses uncoated material. That means the steel is the product and the surface is the steel — there is no metallic coating applied after rolling and no organic coating over it. It also addresses a particular family of flat product, intended for cold forming, within the form and dimensional range the standard itself sets out.
For a quality lead, the practical consequence is that the applicability question has to be answered by a person reading the standard, not by the coil's description in a quotation. "Cold rolled coil" is a description that fits coated and uncoated material, wide and narrow product, forming stock and non-forming stock. The standard is narrower than the description.
Where a scope error comes from
Almost always from the quotation rather than the mill. A supplier quotes "cold rolled coil to EN 10130" from a product family listing, and the buyer accepts it because the material they received last time looked right. The standard was never opened to check whether the product form, the surface condition and the delivered range actually sit inside it. That gap is invisible until quality asks for the applicability basis.
All four must be true
- Cold rolled, not hot rolled. The material has been cold reduced after pickling, so it carries the dimensional consistency and surface character that come from that route rather than the scale and tolerance behaviour of hot rolled product.
- Uncoated. No metallic coating and no organic coating. The surface is bare steel, which is precisely what the standard's scope assumes.
- Low carbon and intended for cold forming. The product is destined for a forming operation — bending, profiling, drawing or pressing — not for structural or wear duty.
- A flat product inside the standard's form and range. The product form and the delivered range fall inside what the standard's own scope clause addresses, which is a reading rather than an assumption.
This is a different route if…
- The material is coated for corrosion protection, so a coating standard governs rather than this one. See the coil standards index
- You need flat product supplied as sheet rather than coil to feed a line. See the steel sheet range
- You are writing the requirement from the material family rather than the process. See EN steel grades
Form & Range
Boundary check before the forming grade goes on the order
Answer four questions about the material itself. The check reports whether the product you are describing sits inside this standard, and which conditions still have to be settled — it states no numeric width or thickness value.
Is this the right standard for this product?
Describe the material as it actually is. The check reports whether it sits inside this standard's family and which order conditions are still unsettled.
This checks whether the product you describe sits inside the standard. It states no numeric width, thickness or mechanical value, and it does not decide whether a particular material suits your forming operation.
Applicability result
Describe the surface condition, how the product form and range were handled, and whether the finish and transit protection are stated. The check reports whether the material is inside the standard and what the order still leaves open.
Nothing here is a specification against a standard, and nothing here states which edition is current. It is a check that the product matches the standard you intend to cite.
Why the width question is not a technicality
Flat rolled steel is produced in forms that differ in how they are made and how they are supplied — a wide coil that feeds a slitting or blanking line, a slit strip that arrives at a particular width, sheet cut from coil. A standard written for a particular family of flat product addresses that family and the range that goes with it. Ordering narrow slit strip and citing a standard for wide cold rolled coil is not automatically wrong, but it is a claim that has to be checked against the standard's scope rather than assumed from the material's appearance. The same logic runs through the thickness range, the surface condition and the edge condition: each is a condition the standard either addresses or does not.

Where It Stops
Four substitutions this standard does not authorise
Each of these is a common shortcut taken when a purchase specification is written from a product list rather than from the standard. Each one moves a decision onto the supplier that belongs to the buyer.
A coated product is bought against this standard
Galvanised and pre-painted coil are frequently described alongside cold rolled material because they start from a cold rolled substrate. The substrate being cold rolled does not make the finished coated product uncoated, and it does not bring the coating inside a standard written for bare steel.
Boundary: the coating changes which standard applies. Cite the document written for the product you are actually buying.
Narrow or slit strip is assumed to be included
A standard addresses a defined family of flat product and the range that goes with it. Taking a conforming wide coil and slitting it to a narrower width produces a different product form, and whether that form is inside the standard is a question for the scope clause.
Boundary: scope is checked for the form you order, not inherited from the form you started with.
Surface finish is treated as a detail the mill will handle
On uncoated cold rolled material the appearance of the surface is a product characteristic customers see. It is also a supply decision that has to be written on the order. A conforming coil with the wrong finish conforms to the standard and still fails your requirement.
Boundary: finish and forming grade are separate order conditions. State both; neither implies the other.
Another system's cold rolled standard is read across
Cold rolled forming grades are written about by more than one standards system, and each organises its designations, its conditions and its test basis differently. The products resemble each other closely, which is exactly why the substitution is easy to make and hard to spot.
Boundary: where the project cites a standard, that standard governs. Moving between systems is a decision, not a lookup.
The common thread: a standard is being asked to cover material it was not written for. The remedy is the same in every case — say what the product actually is, in the terms the standard uses, and let the application be decided rather than inferred. Where a coated product is genuinely required, the correct move is to cite the standard that governs coated material, not to cite this one and hope the coating is overlooked.
Delivery Conditions
What the purchase order has to carry for cold rolled forming feed
A quotation built on a product description rather than an order leaves every one of these to the supplier's default. These are the fields the mill works to — anything missing is decided somewhere you are not looking.
| Order field | What it decides |
|---|---|
| Confirmation the product is uncoated | Whether the standard applies at all. A cold rolled description covers coated and uncoated material, so the surface condition has to be stated rather than assumed. |
| Thickness and width, with tolerances | The delivered size band inspection will accept or reject against. A nominal figure alone gives the receiving check nothing to work with. |
| Forming grade and surface finish | Two separate conditions. The grade governs how the material behaves in your operation; the finish governs what the surface looks like when it arrives and after forming. |
| Edge and dimensional condition | Whether the material arrives in a form your line can accept without further processing, and what the strip edge is expected to be. |
| Coil geometry and quantity | Inner diameter, outer diameter, mass range and total quantity, which determine whether the coil fits your decoiler and how the campaign is scheduled. |
| Surface protection for transit and storage | Whether the coil is oiled and how it is wrapped. Bare steel is the most exposed to handling damage and humidity between the mill and your line. |
| Destination and delivery terms | The document set the receiving inspection expects and the handling the shipment needs on the route in. |
| Tests and certificate type required | What is demonstrated at acceptance and against which basis, so the evidence produced matches what your own inspection will run. |
Related standards and grades on this route
Releasing cold rolled feed to a line
- Confirm the certificate cites the standard and the edition your order invoked, not the number alone.
- Check the surface condition recorded on the documents matches the uncoated product you specified.
- Verify the finish shown against what your formed part has to look like — conformance to the standard does not by itself meet an appearance requirement.
- Compare the delivered thickness and width against the tolerances on your own order, not against a nominal figure.
- Record whether the coil was oiled and how it was wrapped on arrival, particularly if surface condition is contested later.
Why quality leads raise the scope question first
A conforming certificate for material that was never inside the standard is not evidence of anything. Establishing applicability at enquiry stage costs one conversation. Establishing it after a coil has been slit, formed and assembled costs a decision about what to do with finished parts — and by then the question has stopped being technical.
GCC Supply
Uncoated cold rolled feed moving into the Gulf
Cold rolled material is the most surface-sensitive product on this route. It arrives bare, so what happens to it between the mill and your line is part of the specification rather than a logistics detail.
United Arab Emirates
Local and re-export enquiries where the uncoated condition and the delivered range are confirmed before the coil is committed.
Steel coil supply for United Arab Emirates
Saudi Arabia
Programme volumes feeding forming lines, where the finish and the forming grade are fixed before the run is scheduled.
Steel coil supply for Saudi Arabia
Qatar
Project supply where appearance is visible in the finished work, so the surface finish belongs on the order rather than in the specification's margins.
Steel coil supply for Qatar
Oman
Port-oriented routes where coil protection for the sea leg is decided with the order, because uncoated material shows every handling mark.
Steel coil supply for Oman
Bahrain
Industrial supply for manufacturers, where the certificate basis and the release check matter as much as the material itself.
Steel coil supply for Bahrain
Kuwait
Manufacturing supply linking coil to line, so geometry and handling are matched to the decoiler and the storage available on site.
Steel coil supply for KuwaitThese pages cover the supply route and enquiry handling for each destination. They do not claim local warehousing, stockholding, a branch presence or a delivery timescale — those are confirmed against your own order. For uncoated cold rolled material, state the surface protection you need for the sea leg and the storage you have at the receiving end. Bare steel exposed to humidity in transit and on site is a condition the buyer controls, not the mill.
Reference Notes
How applicability is established, and why the quotation is not evidence
A standard sets out requirements for a defined family of product. Whether your material is inside that family is a reading you perform, not a property the material carries.
A cold rolled description is not a scope finding
Cold rolling is a production route and it produces a wide family of flat products — coated and uncoated, wide and narrow, forming grades and non-forming grades. A standard addresses a defined part of that family. Whenever a specification makes the leap from the route to the standard in one step, the scope clause has been skipped.
The scope clause is the first thing a quality lead reads
The scope statement says which products and conditions the standard addresses. It is short, it is near the front of the document, and it settles more disputes than any table further in. Reading it against the actual product takes minutes and prevents the situation where material arrives conforming to a standard that never applied to it.
Surface condition and coating are different properties
Uncoated material still has a surface condition — the finish produced by rolling and the way it is protected afterwards. Coating is the application of another material on top. A standard can address the first while saying nothing about the second, which is why a coated product cannot be brought into an uncoated standard's scope by pointing at the substrate underneath.
Applicability is recorded, not remembered
The check that matters at release is not whether somebody once considered applicability, but whether the decision is written down where the receiving inspection can find it — which edition was read, which product form was confirmed, and what was excluded. That record is what turns a judgement into an auditable basis.
This page states no numeric width, thickness or mechanical value, and no surface roughness figure, because those belong to the edition your contract invokes and they change when it is revised. It also makes no claim about which edition is currently published — that is read from the publisher's own catalogue, which is the only source that stays accurate as the standard is maintained. Read the scope clause of your edition before you apply this standard to a product.
Which question each check answers
Surface condition
Whether the standard applies at all — uncoated material is inside it, coated material is not.
Product form and range
Whether the form you are buying sits inside the family and dimensions the standard addresses.
Forming grade
How the material behaves in your operation, which is a separate question from what it looks like.
Surface finish
What the surface of the finished part has to look like, which conformance alone does not deliver.
Protection and documents
How the material survives the journey, and what evidence proves it met the basis the order named.

FAQ
Uncoated, scope and finish questions
Can I use this standard for galvanised or pre-painted coil?
No. The standard addresses uncoated material, where the surface is the steel itself. A metallic-coated or organically-coated product is a different requirement governed by a different document, and citing this standard for it does not make the coating comply with anything.
Does every cold rolled coil fall inside this standard?
No. Applicability depends on the product form and the range the standard itself sets out, including dimensions and condition. A cold rolled strip outside the width the standard addresses, or produced for a purpose it does not cover, is not brought inside it by sharing the description 'cold rolled coil'.
What is the difference between the surface finish and the forming grade?
They answer different questions. The forming grade relates to what the material has to do in your press or roll former. The surface finish relates to what the surface has to look like when it arrives and after forming. Both are order conditions, and neither substitutes for the other.
Do I need to state delivery conditions on the order?
Yes, where the standard provides for them. Oiling, surface condition and the edge or dimensional condition you need are supply decisions that have to be transmitted deliberately, because the mill produces to what the order says rather than to what the drawing implies.
What has to be settled before a quotation is useful?
Confirm the product is uncoated and inside the standard's form and range. Then fix the thickness and width with tolerances, the forming grade and the surface finish, the coil geometry and quantity, the surface protection you need in transit, your destination and the documents and tests the project requires.
Where It Is Used
Situations where the uncoated condition has to be confirmed
Cold rolled forming feed is bought against downstream processing, so the applicability question usually surfaces at the point where the material is matched to a line.
A specification mixes coated and uncoated line items
One purchase specification covers several components, some needing corrosion protection from the coil and some not. The uncoated items are this standard's territory; the coated ones are not.
Material is bought wide and slit before forming
The coil arrives at one width and reaches the line at another, so the question of which form the standard was applied to has to be settled before the slitting order is placed.
A customer rejects a formed part on appearance
The material conformed and the part still failed, because the surface finish requirement was never written on the order — conformance and appearance are different conditions.
A new line is commissioned and needs a released material basis
The line is specified for a range of feed, and the quality function has to state which standard each part of that range is bought against before production starts.
Stock is transferred between projects
Material bought for one job is held for another, and somebody has to confirm the uncoated condition and the recorded basis still hold for the second use.
A supplier quotes a familiar description
The quotation says cold rolled coil and names the standard, and the buyer has to decide whether that description actually establishes applicability before accepting it.
Where a coated product belongs instead
If the application needs corrosion protection from the coil itself, the material is a coated product and the governing document is the one written for that coating. The application route below sets out the requirement from the end-use side, which is the more reliable starting point when the decision is driven by what the finished component has to withstand rather than by the steel beneath it.
Coated coil for roofing and cladding applicationsWhere the decision leads next
SPCC cold rolled coil
If the requirement is being written against a grade designation rather than a standard, this is where the grade sits.
See SPCC coilASTM A1008 cold rolled coil
If the project cites the ASTM system for the same cold rolled forming duty, start from that route instead.
See A1008Steel coil standards
The other standards this route is ordered against, if the governing document is still being decided.
See coil standardsRequest a Quote
Send the thickness and width with tolerances, confirmation that the material is uncoated and for forming, the forming grade and surface finish you need, the edge condition, the coil geometry and quantity, the surface protection required for transit, your destination, and the tests or certificates the project calls for. Price is on request.
Cold rolled enquiries on this route are handled through the steel coil desk — the main steel coil enquiry desk. The form here reaches the same team.
Office 3303, Churchill Executive Tower, Business Bay, Dubai, United Arab Emirates
Monday – Saturday: 8.00 AM – 6.00 PM · Sunday: Closed