
ASTM A706 Grade 60 Rebar
ASTM A706 Grade 60, Specified For A Reason
A706 Grade 60 is a different specification, not a stronger or softer A615. It is written around controlled chemistry, restricted carbon equivalent, measured ductility and a defined tensile-to-yield relationship, which is why projects whose detailing depends on those properties specify it. What it is not is an automatic seismic pass: the grade name carries no seismic approval, and whether your structure qualifies depends on the ductility class and detailing provisions in the structural code your project has adopted. Confirm the A706/A706M edition, the grade designation, the continuity and detailing requirements the code sets, and the per-lot ductility evidence before the enquiry is issued.
What the grade name does not do
- It is not a seismic approval for any structure.
- It is not interchangeable with A615 Grade 60.
- It does not qualify a weld or fix a lap length on its own.
Information current as of
When A706 Is The Right Route
Same strength number as A615 Grade 60. Different specification entirely.
A706 is specified when the design leans on properties A615 does not control in the same way — restricted chemistry, a defined ductility and tensile-to-yield relationship, and welding provisions that make fabricated splices a practical route. The options below are grouped by the reason you would choose or rule each out. None of them is a strength comparison, and the A706 grade name is never a substitute for your code's qualification.
ASTM A706 Grade 60 rebar
Current specificationChoose it when
When the design depends on controlled chemistry, measured ductility and a defined tensile-to-yield relationship — typically where the detailing code's continuity and splice provisions are written into the design, or where welded splices are intended.
Before you commit
The grade name carries no seismic approval. Whether the structure qualifies is determined by the ductility class and detailing provisions of the code your project adopted, confirmed by your structural engineer.
ASTM A615 Grade 60 rebar
Same strength, different specificationChoose it when
Where the design does not rely on A706's controlled chemistry or ductility provisions and standard carbon-steel bar to A615 is specified.
Before you commit
A shared strength number is not a shared specification. Chemistry limits, ductility framework and welding provisions differ, and the detailing that depends on them does not carry across.
Compare this specificationASTM A706 rebar (standard overview)
The specification routeChoose it when
Orient the A706 decision inside the specification itself — its scope, its chemistry framework and how it differs from carbon-steel bar.
Before you commit
The overview is orientation, not acceptance. Your project's edition and design code still decide what may be supplied and how it may be detailed.
Compare this specificationASTM steel grades
Cross-product taxonomyChoose it when
Compare the A706 grade decision against the wider ASTM grade reference before assessing designations across product families.
Before you commit
The reference is orientation, not acceptance, and it does not establish that any grade is suitable for a structure.
Compare this specificationWhat A706 actually controls
Chemistry within restricted limits, a defined carbon equivalent, and a mechanical framework that includes a tensile-to-yield relationship rather than strength alone.
Why that matters to detailing
Design provisions that depend on ductility, continuity and splice behaviour need reinforcement whose properties are controlled in those terms — which is what the specification provides.
Where the specification stops
At the material. Whether your member satisfies a ductility or seismic requirement is a code-based determination your structural engineer makes against the structure, not something a bar designation confers.
The specification rule
Specify A706 because the design depends on what it controls — not because it is a stronger or safer-sounding bar. Confirm that the structural code your project has adopted assigns the ductility and detailing provisions you are relying on, that the bar size you need is carried at this grade in your edition, and that any welded splice has a procedure and qualification behind it. Substituting A615 removes the basis for those provisions rather than saving cost, and no bar designation on its own qualifies a structure.
Ductility & Welding Evidence Planner
Establish the specification, then prove the design basis behind it
This planner follows the A706 decision rather than a procurement list: it holds at 'verify first' until the bar size is stated, then will not clear until you have named the ductility class and detailing basis the design relies on. Selecting an A615 edition against this specification returns a conflict, because the shared strength number is not a shared specification.
Specification & design-basis inputs
Required fields marked *Use the edition the project or purchase specification requires.
Confirm the size is carried at this grade in your edition.
Commit to one ordered system per lot; label any conversion informational.
State the code basis the A706 route rests on — the planner will not clear without it.
Required test / document evidence
Nominal mass refers to the base bar and is either supplied by you or confirmed against the governing standard and the supplied MTC. This planner does not estimate weight, does not qualify a weld, does not provide lap lengths, and does not certify a structure.
Specification check
Add the governing A706 edition next
The grade is set; the edition fixes the chemistry limits, the mechanical requirements and the test framework that apply. State the edition — for example ASTM A706/A706M-26, or the earlier edition the project names.
For the engineer to close
- The ductility class your adopted code assigns to the members in question.
- The continuity, lap-splice and anchorage provisions the code sets for those classes.
- Whether the design relies on welded splices, couplers or standard laps.
- The welding procedure, filler class and qualification the design requires.
- The inspection and testing hold points the project imposes on the supplied lot.
What this specification does not claim
- The A706 grade name is not a seismic approval. Whether a structure qualifies depends on the ductility class and detailing provisions in the code your project adopted — that determination is your structural engineer's, against the governing code.
- A706 Grade 60 and A615 Grade 60 share a strength number but not a specification. They are not interchangeable, and the chemistry, ductility and welding frameworks differ.
- A706's controlled chemistry supports welding provisions, but it does not by itself qualify a weld. The procedure, filler and qualification remain separate requirements.
- The permitted bar-size set and the edition both matter — confirm the size is carried in the edition your project is bound to.
- Measured ductility on the supplied heat is evidence. The designation alone is a requirement.
Nothing is transmitted yet, and this planner does not qualify your structure for any design case. When the design-side basis is on record, send the summary to the commercial department for a confirmed quotation.
Standard, Grade & Specification Route
What A706 defines, and what your design code still has to decide
The specification fixes the chemistry limits, the mechanical framework and the permitted sizes. It does not fix the ductility class your structure must satisfy, the lap and splice provisions that follow from it, or the qualification behind a welded joint. Read the tables in that order — that is the order the decisions bind.
Specification identity
Which specification governs — and which similar-looking one does not
| Standard / grade | Applicability & limitation | What it means for your design | Enquiry field / next action |
|---|---|---|---|
| ASTM A706/A706M Grade 60 [420] | A low-alloy reinforcing-bar specification with controlled chemistry, restricted carbon equivalent and a mechanical framework that includes a tensile-to-yield relationship, carried in its own permitted size set. | Supports design provisions that depend on controlled ductility and splice behaviour — the material basis your detailing leans on. | State the edition, grade and permitted size. |
| ASTM A615/A615M Grade 60 [420] | A carbon-steel specification sharing the strength number but not the chemistry limits, ductility framework or welding provisions. | Not a substitute. Detailing that depends on A706's controlled properties loses its basis if the bar is swapped. | Confirm the governing specification explicitly. |
| A706 at another grade | A706 carries more than one grade designation, each with its own requirement in the edition in force. | A different grade number is a different requirement — moving between them reopens the mechanical and detailing checks. | State the exact grade the design specifies. |
| Non-ASTM national grades | Strength and ductility labels in other national standards describe different frameworks and test regimes. | A similar-looking label carries no chemistry, ductility or welding equivalence and does not establish splice behaviour. | State the governing standard and grade. |
The table states specification scope from public standard information. Confirm the exact edition and its requirements against the current standard documents before specifying — no unsupported numeric values are published here.
Ductility, splicing & welding
The decisions that make A706 worth specifying — and the ones it cannot make for you
| Decision | Applicability & limitation | What it means for your design | Enquiry field / status |
|---|---|---|---|
| Ductility class & code qualification | Determined by the structural code your project has adopted and the member in question — not conferred by the bar designation. | A706 provides the material basis; your engineer establishes whether the member satisfies the code's class requirements. | Confirm the adopted code and class. |
| Continuity & lap splices | Provisions follow from the code and the ductility class, applied to the actual layout, bar size and congestion. | Confirm splice locations and lengths are calculated for this grade and your code basis, not copied from another project. | Confirm splice detailing on record. |
| Welded splices & couplers | A706's controlled chemistry is what makes welding a practical route, but procedure, filler class, joint detail and qualification are separate requirements. | State the required welding procedure and qualification; the material does not qualify the joint on its own. | State welding + qualification requirement. |
| Tensile-to-yield relationship | A controlled mechanical property within the specification's framework, measured on the supplied heat. | Where the design relies on it, require the measured results rather than accepting the designation as evidence. | Request mechanical results on the heat. |
| Chemistry & carbon equivalent | Restricted within the specification, and reported for the actual heat on the mill certificate. | Confirm the chemistry information required by your project is issued against the delivered lot. | Request chemistry & carbon equivalent. |
No lap length, carbon-equivalent limit or mechanical value is published on this page. Each is a function of your grade, bar size, concrete, code basis and the edition in force, and belongs with your structural engineer and the current standard.
Bounded comparison
The adjacent routes worth opening before you commit
Each route answers a specific neighbouring question — the carbon-steel specification sharing this strength number, the A706 specification itself, and the lap guidance your detailing depends on. None of them is interchangeable with your requirement unless the design authority approves the change.
The A706 specification
Open referenceA615 Grade 60 — same number, different spec
Open referenceASTM A615 — the carbon-steel route
Open referenceLap length guidance
Open referenceComparison is bounded to the stated specification, grade and size basis. A shared strength number does not make A615 and A706 Grade 60 equivalents, and neither substitutes for the other without approval.

Welded splices
Controlled chemistry makes welding viable. It does not make the joint qualified.
Welding reinforcement is one of the main reasons A706 gets specified, because its restricted chemistry and carbon-equivalent limits make the material far more amenable to it than general carbon-steel bar. The step that is routinely skipped is the one that matters: the welding procedure specification, the filler class, the joint detail and the welder qualification are requirements in their own right, and they sit alongside the material certificate rather than being satisfied by it. Where your design depends on welded splices, state the procedure and qualification you require on the enquiry. The imagery here illustrates the fabrication step; it is not evidence of a qualified procedure.
Acceptance & Evidence
What makes one A706 quote comparable with another
At this specification the paperwork carries the design: the whole point of A706 is that specific properties are controlled and measured. State what you require up front, and keep the specification's requirements separate from what the delivered heat actually achieved.
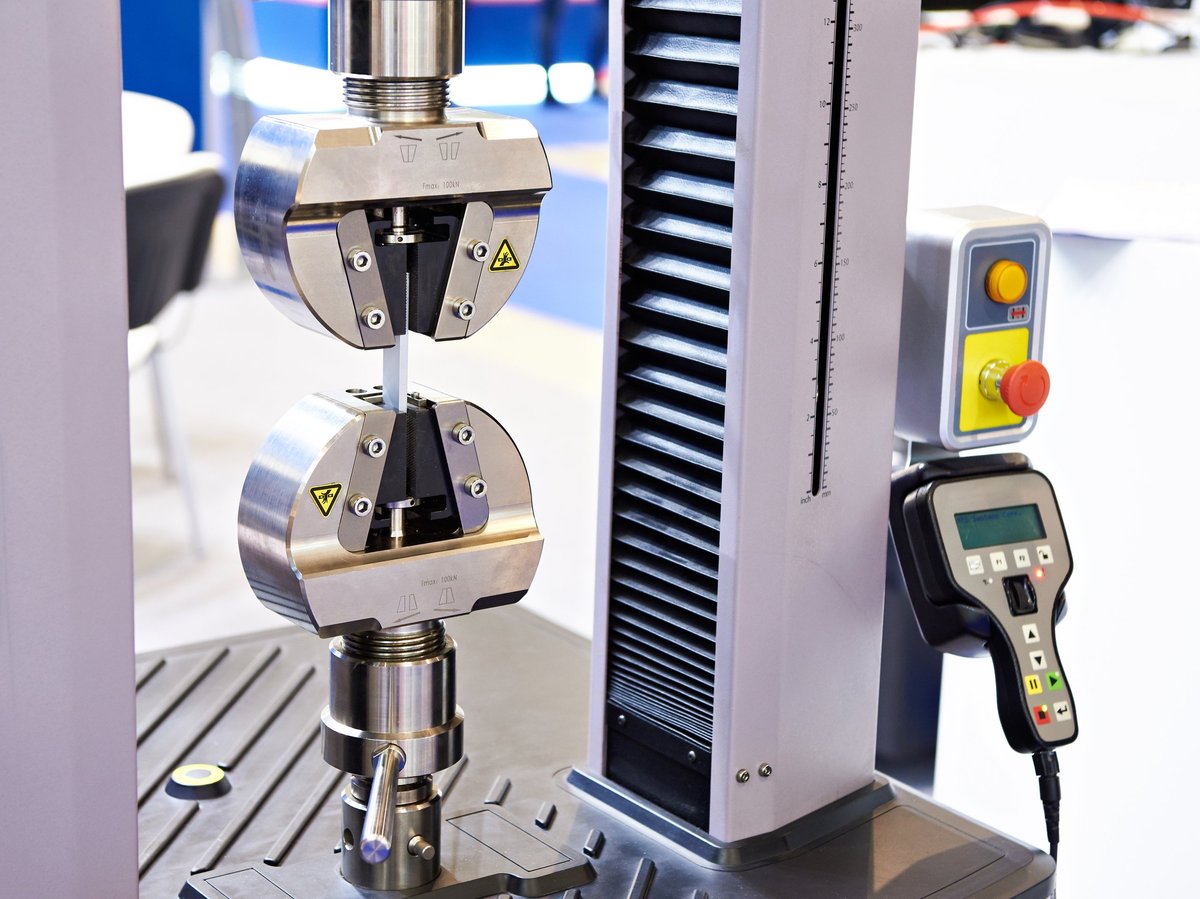
| Evidence / document | What it verifies | When it is required | Enquiry action |
|---|---|---|---|
| Mill Test Certificate (MTC / EN 10204 3.1) | Identity, chemistry and mechanical results for the heat that produced the bar lot. | Where the project requires certified material — effectively always where the design leans on controlled properties. | Request at enquiry; content confirmed against the delivered lot. |
| Chemistry & carbon-equivalent information | The chemistry of the supplied heat against the specification's restricted limits. | Where the design or the welding procedure depends on chemistry being within controlled limits. | Request chemistry and carbon equivalent for the heat. |
| Tensile, yield & elongation results | The measured mechanical performance of the heat, including the relationship the specification controls. | Where the design relies on ductility or the tensile-to-yield relationship rather than on strength alone. | Request results tied to the heat. |
| Bend / rebend results | Bend acceptance of the lot at the diameters the detailing uses. | Where the detailing approaches the minimum bend diameter or the project requires bend evidence. | Request results at the scheduled diameters. |
| Welding procedure & qualification records | That the welded splices used have a specified procedure, filler class and qualified welders behind them. | Where the design relies on welded splices rather than standard laps or couplers. | Provide from the fabricator; accompanies the material certificate. |
| Designer's ductility & detailing record | The ductility class and continuity, splice and anchorage provisions applied to this member. | Where the code constrains the member or an authority requires the design basis on file. | Provide from the designer; not a supplier document. |
Standard vs supplied lot
The specification sets the requirement; the mill certificate evidences the delivered heat. Where the design leans on controlled properties, the second is what it rests on.
Issued on test
Certificates and test records are issued against the actual delivered lot — they cannot be asserted in advance of it.
Design-side record
The ductility class, splice provisions and welding qualification sit with your designer and fabricator, not with the supplier's documentation.
Rebar lap length guide
Work through how lap and splice length is arrived at for your grade, bar size and code basis — and why it is not a fixed table value.
Open technical referenceRebar chemical & mechanical properties
See how yield, tensile, elongation and chemistry requirements are framed for a specified grade, and what the mill certificate must evidence.
Open technical referenceWhere This Specification Gets Specified
The applications where controlled ductility and splicing provisions drive the choice
These are the settings where an A706 route is most often taken — continuity and dynamic demand in bridges, repeated loading and joint detailing on road and infrastructure work, and densely reinforced and tightly toleranced linings in tunnels. Each states the limit that still has to be confirmed.
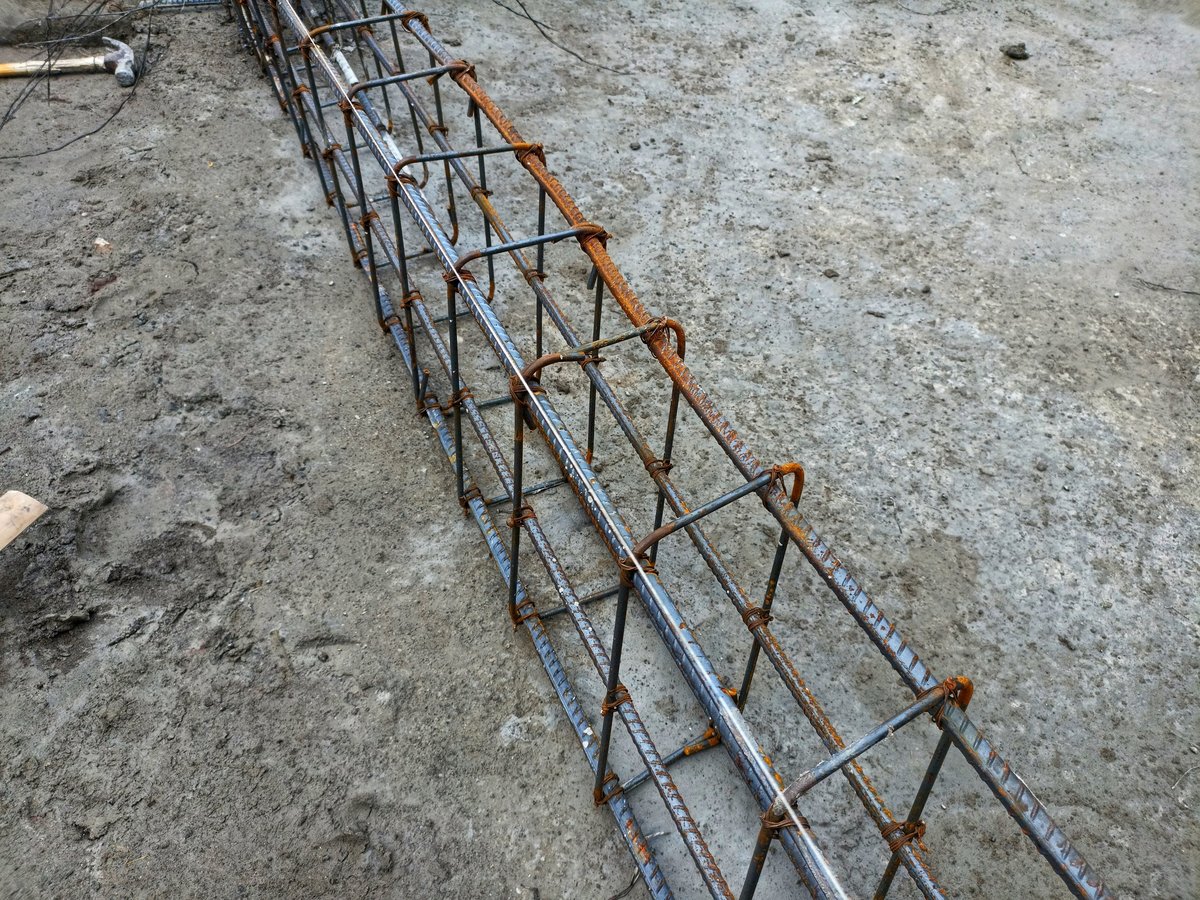
Bridge rebar
Where it drives the choice
Bridges combine dynamic loading, exposure and heavy continuity detailing — the conditions where a ductile specification and its splice provisions most often drive the bar choice.
Fit limit
The bridge's governing design code and durability class are confirmed from the project; this page does not certify a bar for a given structure.
Open applicationRebar for road construction
Where it drives the choice
Road and infrastructure work brings repeated loading and joint detailing, where continuity and lap provisions interact with the specification rather than standing apart from it.
Fit limit
The pavement or structure type and its code basis come from the design, and are confirmed against it.
Open applicationTunnel rebar
Where it drives the choice
Tunnel linings are densely reinforced with demanding fixing tolerances, which makes lap and splice detailing a live constraint on the specification route.
Fit limit
Detailing capacity at the congested section is confirmed by the designer against the code provisions in force.
Open applicationApplication fit is confirmed against the governing specification, the permitted bar size, and the design code in force when the enquiry is quoted. No generic or unsupported suitability claims are made on this page.
GCC Markets & Destination Planning
Plan the destination, evidence and delivery basis for an A706 enquiry
For each GCC destination the specification, documents and commercial terms are aligned to your project basis at quotation. Availability and delivery are confirmed from your complete specification — never claimed in advance.
United Arab Emirates
Technical submittal and welding-procedure review.
Add the delivery location, importer/customs inputs, Incoterm and document set before the A706 enquiry is issued.
Saudi Arabia
Large EPC quantities and cross-border documentation.
Confirm the delivery location, importer inputs, Incoterm and documents so a ductile-specification enquiry is quoted on one consistent basis.
Qatar
Infrastructure technical-approval readiness.
Add the technical submittal and document package the project requires for a controlled-chemistry bar.
Kuwait
Contractor and fabricator hand-off.
State the delivery location, Incoterm, documents and required date so the order can be planned against the specification basis.
Bahrain
Contractor procurement and industrial supply.
Provide destination, importer/customs inputs, Incoterm and documents before quotation of the A706 rebar.
Oman
Port-oriented project supply planning.
Confirm the destination, required documents and Incoterm so the quotation basis is fixed for the specified grade.
Destination, documents, port or delivery line, Incoterm and the required delivery date are fixed at quotation from your specification. No served markets, local stock, local branches or delivery times are claimed in advance.
Commercial & Availability Inputs
What turns an A706 specification into a confirmed offer
Availability, packing, documents, Incoterm and delivery are agreed from your full specification. Price is always on request — no live stock, lead-time or pricing claims are made before quotation.
| Quotation input | What it fixes | Status |
|---|---|---|
| Governing edition & grade | Which A706/A706M edition and which grade designation the offer is made against. | Required before quotation. |
| Bar size & permitted-size check | The nominal size and confirmation that it is carried at this grade in the edition. | Required before quotation. |
| Design basis | The ductility class and continuity/splice provisions the specification route rests on. | Required before the enquiry is issued. |
| Welding requirement | Whether welded splices are used, and the procedure and qualification required. | Required where welding applies. |
| Quantity & unit | Total tonnes or bar count for the schedule. | Required for quotation. |
| Packing & bundle marking | Bundled, strapped and tagged with size, grade and heat marking. | Confirmed from the order. |
| Inspection & documents | The MTC plus chemistry, carbon-equivalent and mechanical records required. | Fixed at quotation per the standard and service. |
| Availability (stock / mill) | Whether the enquiry is met from current availability or scheduled production. | Confirmed at quotation — never claimed in advance. |
| Incoterm & named place/port | The commercial and delivery basis for the consignment. | Fixed with the destination. |
| Required date | The delivery window the programme depends on. | Confirmed against availability. |
Price, stock, lead time, mill/origin and routing are quotation-dependent unless current verified evidence is present.
Commercial department
The commercial desk checks each A706 enquiry for edition and grade consistency, confirmation that the bar size is carried at this grade, the design basis behind the specification route, the welding requirement where it applies, the required document set and the delivery basis before quoting. Continue to the exporter route when packing, named place, Incoterm, export-document and shipment-planning fields are needed.
Steel rebar exporterOffice 3303, Churchill Executive Tower, Business Bay, Dubai, United Arab Emirates
Monday – Saturday: 8.00 AM – 6.00 PM · Sunday: Closed
Verifiable Outcomes
What each concern is checked against, and what you can rely on
Each risk on this page is mapped to the check that actually addresses it, then to a practical procurement outcome. No superiority claims and no structural-suitability claims are made.
| Buyer concern | Check on this page | Outcome you can rely on |
|---|---|---|
| Reading a seismic approval into the grade name | The planner states explicitly that A706 carries no seismic approval and holds the result until the design code's ductility class is stated. | The code-based qualification question is raised by the engineer, not assumed from the bar mark. |
| Treating A615 Grade 60 as an A706 substitute | Selecting an A615 edition against this specification returns a conflict rather than a pass, with the specification difference set out. | The swap is caught at specification stage, before chemistry and ductility evidence go missing. |
| Assuming A706 chemistry qualifies a weld | The planner separates the material's welding provisions from the procedure, filler and qualification the design still requires. | Weld qualification is treated as its own requirement rather than inherited from the bar. |
| Accepting ductility from the designation instead of the lot | The evidence matrix requires the chemistry and ductility results tied to the supplied heat, separate from the standard's requirement. | Ductility compliance is demonstrated on the delivered lot, not inferred. |
| Leaving splice and lap provisions to the fabricator | Continuity, lap-splice and anchorage provisions are surfaced as design-code inputs the engineer must close. | Detailing provisions are settled in design rather than discovered at fixing. |
From design intent to delivery
- 1
Establish why A706 is required
Confirm the design genuinely depends on A706's controlled chemistry, ductility and splice provisions rather than specifying it by habit.
- Owner:
- Structural designer
- Input:
- Design intent and governing standard
- Output:
- Confirmed specification route
- Risk:
- A706 chosen without a reason
Next: Identify the ductility class the code assigns
- 2
Identify the code's ductility class
Determine which ductility class your adopted detailing code assigns to the members, and what it requires of the reinforcement.
- Owner:
- Structural designer
- Input:
- Adopted code, member type
- Output:
- Ductility class and its provisions
- Risk:
- Seismic suitability assumed from grade name
Next: Close the continuity and splice detailing
- 3
Close continuity, lap and anchorage detailing
Apply the code's continuity, lap-splice and anchorage provisions to the actual layout, bar size and congestion.
- Owner:
- Designer + detailer
- Input:
- Layout, bar size, congestion
- Output:
- Compliant detailing
- Risk:
- Lap lengths assumed rather than calculated
Next: Resolve the welding requirement
- 4
Resolve the welding and splicing requirement
State whether the design relies on welded splices or couplers, and what procedure, filler class and qualification it requires.
- Owner:
- Designer + fabricator
- Input:
- Splice type, welding procedure
- Output:
- Welding/splicing requirement
- Risk:
- Material chemistry read as weld qualification
Next: Define the acceptance evidence set
- 5
Define the acceptance evidence set
State the chemistry, carbon-equivalent, tensile and elongation evidence required against the supplied heat, in the ordered unit system.
- Owner:
- Buyer + inspector
- Input:
- Required documents and tests
- Output:
- Per-lot evidence set
- Risk:
- Designation substituted for results
Next: Fix destination and commercial terms
- 6
Fix destination, Incoterm and date
Confirm the delivery location, Incoterm rule and required date so the enquiry is complete and comparable.
- Owner:
- Buyer + commercial
- Input:
- Destination, Incoterm, date
- Output:
- Qualified enquiry ready to issue
- Risk:
- Unstated evidence or port
Next: Issue the qualified RFQ
Technical reference note
Which authoritative requirement most changes an A706 Grade 60 decision
A source-backed note on the requirement this page is built around — stated with its source, its checked date and its limits.
The requirement that changes the decision
The single fact that governs most A706 decisions is that the specification controls properties which the general carbon-steel rebar specification does not control in the same terms. ASTM A706/A706M sets chemistry within restricted limits, places a limit on carbon equivalent, and frames its mechanical requirements around a relationship between tensile and yield rather than a strength figure alone. For a designer, that is the point: detailing provisions that depend on ductile behaviour and predictable splice performance need reinforcement specified in those terms, and welding becomes a practical fabrication route rather than a marginal one.
The consequence that gets missed is the boundary. The material specification does not tell you what your structure must satisfy. The ductility class a member has to meet, the continuity and lap-splice provisions that follow, and whether the design relies on welded joints — those come from the structural code your project adopted, applied to the specific structure. A conforming consignment and a qualifying member are two separate demonstrations, and a mill certificate evidences only the first. Where a project requires weld qualification, that too is a separate record, sitting alongside the material certificate rather than being satisfied by it.
Primary authority
ASTM International — ASTM A706/A706M, Standard Specification for Deformed and Plain Low-Alloy Steel Bars for Concrete Reinforcement — store.astm.org/a0706_a0706m-23.html
Checked · confirm the current active edition on the publisher's site
What this note does and does not cover
Covers: the A706 specification's scope, its controlled-chemistry framework and the separation between the material specification and the project's structural design code.
Does not cover: your adopted structural code, the ductility class applicable to your members, or national standards outside ASTM — each is a separate authority you must consult directly.
Limit: the public ASTM page is a scope and abstract reference, not a substitute for the purchased full standard. Nothing here asserts seismic suitability, qualifies a weld, or provides a lap length for any structure.
Practical consequence: confirm the edition and the permitted size against the specification, confirm the ductility class and splice provisions against your adopted code, and require lot-specific chemistry and mechanical evidence before acceptance.
FAQ
The questions that come up before an A706 bar is specified
Written for the engineer weighing the specification route as much as for the buyer raising the enquiry.
Does specifying A706 Grade 60 make my structure seismic-compliant?
No. A706 is specified because its controlled chemistry, ductility and tensile-to-yield requirements support detailing that depends on those properties. Whether a structure satisfies a seismic design requirement is determined by the ductility class and detailing provisions of the code your project has adopted, assessed by your structural engineer. The grade name is not an approval, and this page does not certify any structure.
Can I use A615 Grade 60 instead of A706 Grade 60?
They share a strength number but not a specification. A706 is a low-alloy designation with controlled chemistry limits and a defined ductility and tensile-to-yield framework; A615 is a carbon-steel specification with its own requirements. If your detailing depends on A706's properties, substituting A615 removes the basis for that detailing. Any substitution needs the structural designer's approval.
Does A706 mean the bar can be welded without further qualification?
No. A706's chemistry framework is what makes welding a practical route, but the welding procedure, the filler class, the joint detail and the welder qualification are separate requirements that still have to be specified and qualified. Treat welding as its own specification field and state the procedure the design requires.
Why can I not just use a standard lap length table?
Because lap and splice length is a function of the grade, bar size, concrete strength, confinement and the design code's provisions — not a single number attached to a bar designation. A table is a starting point for understanding the variables; the length used in your detailing has to be calculated for your structure. Your engineer's detailing governs.
What evidence should I require for an A706 consignment?
Ask for the mill test certificate covering the supplied heat, including the chemistry and carbon-equivalent information and the tensile and elongation results your project requires, tied to the actual lot and stated in the ordered unit system. Where welded splices are used, the welding qualification records sit alongside this rather than replacing it.
Is A706 available in the same bar sizes as A615?
Do not assume the size sets are identical. Each specification carries its own permitted sizes, and the edition your project is bound to matters as well. Confirm the bar size in your design is carried at A706 Grade 60 in that edition before the detailing is finalised, so a late size change does not reopen the splice calculations.
Qualified RFQ
Request a quote for ASTM A706 Grade 60 Rebar
Copy the RFQ summary you have built, then send it to the commercial department. The enquiry is ready for review once the edition, grade, permitted bar size, ordered unit system, design basis, quantity, destination and required evidence are complete.
Price, stock, origin and lead time remain quotation-dependent unless current verified evidence is present. This page does not assert seismic suitability, qualify a weld or provide lap lengths.
Office 3303, Churchill Executive Tower, Business Bay, Dubai, United Arab Emirates
Monday – Saturday: 8.00 AM – 6.00 PM · Sunday: Closed
Copyable RFQ summary
- Standard / edition
- To be confirmed
- Grade
- Grade 60 [420]
- Bar size / designation
- To be confirmed
- Ordered unit system
- To be confirmed
- Design basis
- Not stated
- Quantity
- To be confirmed
- Destination
- To be confirmed
- Nominal mass (kg/m)
- Confirm per standard / MTC
Add any remaining open items — permitted-size confirmation, the code's ductility class, splice provisions, welding qualification, availability, price, origin or lead time — as explicit fields before sending.